
Reducing manufacturing costs sounds straightforward until the proposed savings begin affecting part quality, durability, or production reliability. A lower resin price may introduce performance concerns. A thinner wall may reduce material usage but compromise strength. A shorter cycle time may improve throughput but create dimensional variation if the process is pushed beyond its stable operating window.
That is why cost reduction in injection molding should focus on eliminating unnecessary expense rather than weakening the requirements that make a part functional.
For procurement and engineering teams preparing next year’s budgets, the most effective cost reduction opportunities often come from design for manufacturability, material evaluation, cycle time improvements, tooling decisions, and simplifying secondary operations.
This guide explains where to look for savings and how to evaluate proposed changes without compromising the critical specifications your program depends on.
Understand the Total Cost Before Making Changes
Injection molding cost includes much more than the resin used in each part. Tooling, machine time, labor, inspection, scrap, secondary operations, packaging, and logistics all influence total manufacturing expense.
A cost reduction strategy should begin by identifying which of these areas contributes most to the current program.
For example, a small component produced in high volumes may have significant opportunities tied to cycle time or cavity count. A larger component may have more savings potential through material usage and wall thickness optimization. An assembly requiring several post-molding operations may benefit from a design that combines multiple functions into a single molded part.
Without understanding the cost structure, teams risk focusing on the most visible expense rather than the one that offers the greatest opportunity.
Hansen’s guide to injection molding cost drivers provides additional context on tooling, resin, machine time, labor, packaging, and other factors that affect the total program budget.
Use Design for Manufacturability to Eliminate Unnecessary Complexity
Design for manufacturability, or DFM, is one of the most useful approaches to reducing molding costs because it addresses problems before they become production expenses.
A part that is difficult to mold may require longer cycles, more inspection, additional tooling actions, or repeated process adjustments. Design changes that simplify manufacturing can help reduce those costs while maintaining or improving performance.
Some common DFM opportunities include reducing unnecessary wall thickness, simplifying complex features, improving draft, eliminating difficult undercuts, and reviewing whether all specified tolerances are functionally necessary.
However, each change should be evaluated against the part’s actual operating requirements. Removing a reinforcing feature may save material, but it is not a useful improvement if the part no longer withstands its intended load.
A detailed injection mold design review can help identify opportunities to simplify geometry while protecting fit, strength, appearance, and other critical requirements.
Optimize Wall Thickness Without Sacrificing Strength
Wall thickness affects material consumption, cooling time, dimensional stability, and the risk of defects such as sink and warpage.
Thicker sections often require more time to cool, which can extend the molding cycle. They also increase part weight and resin consumption. For some designs, reducing unnecessary thickness can improve both part quality and manufacturing efficiency.
The key is to evaluate how loads move through the component. Rather than adding material everywhere, engineers may be able to improve stiffness through appropriately designed ribs, gussets, and support features.
Smooth transitions between wall sections can also help reduce uneven shrinkage and internal stress.
These changes should be reviewed alongside material properties, impact requirements, assembly loads, and expected service conditions. In some applications, a thicker wall is necessary. In others, geometry can provide the required strength more efficiently.
Review Resin Selection Based on Actual Performance Requirements
Material selection creates another potential opportunity for cost reduction. A component may have been specified with an engineering resin because of an earlier design requirement that has since changed. Alternatively, the current material may provide performance properties beyond what the application requires.
Before considering a lower-cost resin, review the component’s actual operating environment. Temperature, chemical exposure, impact, UV exposure, wear, and dimensional stability should all be considered.
A resin with a lower purchase price is not necessarily less expensive to manufacture. It may require different processing conditions, create greater scrap risk, or introduce performance concerns that increase total program cost.
Similarly, a higher-priced material may offer better economics if it reduces defects, improves processing consistency, or supports a more efficient design.
Any proposed material substitution should be evaluated through engineering review and appropriate validation before being introduced into production.
Cycle Time Improvements Can Produce Meaningful Savings
Cycle time determines how frequently a mold can produce finished parts. When production volumes are high, even modest improvements can reduce the amount of machine time required to meet demand.
However, cycle time optimization should never be treated as simply running the machine faster.
Cooling, filling, packing, and ejection all influence part quality. Reducing cooling time too aggressively may contribute to warpage or dimensional instability. Changes to packing conditions can affect shrinkage, sink marks, and critical dimensions.
A more effective strategy is to evaluate the full molding process and identify where time can be reduced without moving outside a validated process window.
For example, improvements to cooling efficiency, material preparation, or ejection reliability may help reduce cycle time while maintaining part consistency.
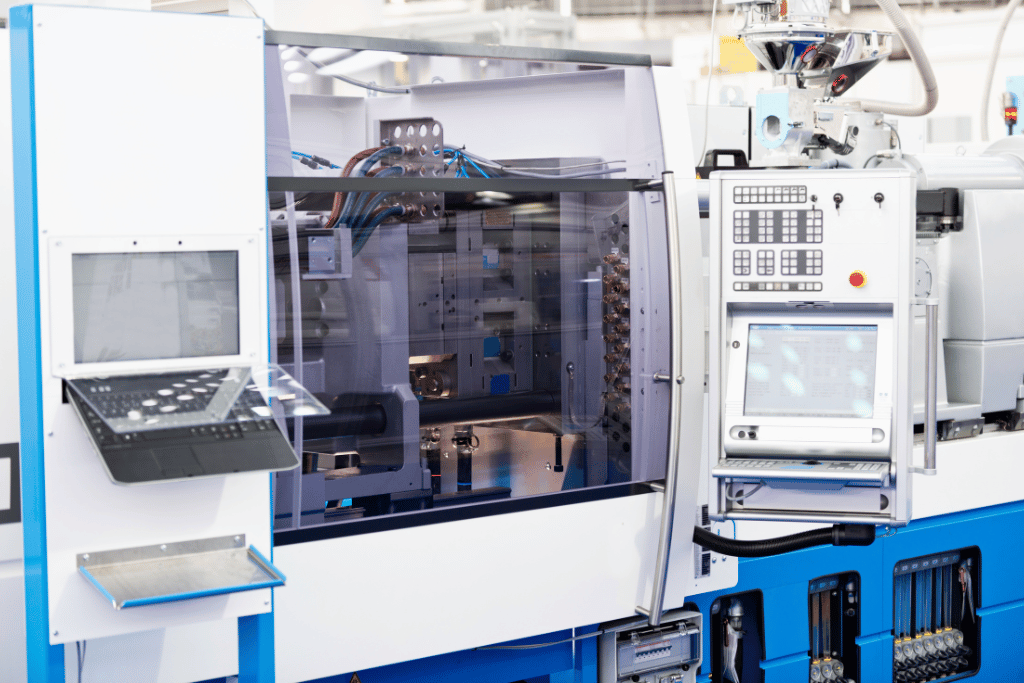
Hansen’s plastic injection molding services include process approaches focused on repeatability, production efficiency, and quality control.
Evaluate Hot Runner and Cold Runner Tooling Economics
Runner systems can influence material waste, tooling expense, maintenance requirements, and cycle time.
A cold runner system generally has a simpler tooling arrangement, but the runner material solidifies and is removed during each cycle. Depending on the resin and program requirements, that material may be reused or treated as scrap.
A hot runner system keeps material molten within heated channels and can reduce runner waste. For higher-volume programs or applications using expensive resin, that reduction may provide meaningful savings over time.
However, hot runner tooling typically requires a higher initial investment and more specialized maintenance. It may not be the best fit for lower-volume programs or certain materials.
When evaluating hot runner vs cold runner tooling, compare the full cost of each approach across the expected production life rather than focusing only on initial tool price or scrap volume.
Reduce Secondary Operations Through Smarter Part Design
Some of the most valuable savings opportunities happen after the part leaves the mold.
Secondary operations such as trimming, drilling, fastening, assembly, decorating, and packaging add labor and handling requirements. Depending on the component, certain operations may be simplified or eliminated through design changes.
For example, a molded-in fastening feature may replace a separate assembly step. A redesigned component may combine functions previously performed by multiple parts. Insert molding may also be appropriate when a program requires durable integrated fastening features.
These approaches can reduce part handling and assembly complexity, but they may also affect tooling costs or design flexibility.
The decision should be based on total manufacturing cost, production volume, and the functional requirements of the finished assembly.
Do Not Reduce Quality Controls Without Understanding the Risk
Inspection and quality documentation are sometimes viewed as opportunities to reduce cost, particularly when teams are reviewing mature production programs.
While inspection plans should be efficient, reducing checks without understanding their purpose can create costly problems.
Critical dimensions, sealing surfaces, fit requirements, and safety-related features may require ongoing monitoring to maintain production consistency.
A more effective approach is to review whether inspection frequency and methods are aligned with actual process capability and customer requirements. Stable production data may help support a more efficient inspection strategy, but any change should be validated and approved where required.
The goal is not fewer inspections at any cost. It is an effective injection molding quality control plan that protects function while avoiding unnecessary work.
Prioritize Cost Reduction Opportunities Based on Risk and Value
Not every proposed improvement should be implemented at the same time. Some changes involve minor process adjustments, while others require tooling modifications, material qualification, or new product testing.
Before approving a cost reduction project, engineering and procurement teams should evaluate four questions:
- What specific cost is the proposed change intended to reduce?
- What investment, validation, or tooling change is required?
- Could the change affect critical dimensions, strength, appearance, or service life?
- How much production volume is needed to recover the investment?
These questions help teams focus on improvements that provide measurable value without introducing disproportionate risk.
Documenting the baseline cost, expected savings, implementation requirements, and validation results also makes it easier to evaluate whether the project delivered the intended outcome.
Cost Reduction Should Improve the Manufacturing Process
The strongest cost reduction initiatives do more than lower the price of an individual part. They improve how the part is designed, molded, inspected, assembled, or delivered.
For OEMs, this means looking beyond material price and identifying opportunities through DFM, cycle time optimization, tooling strategy, resin selection, and secondary operation improvements.
These changes work best when procurement and engineering collaborate early and when performance requirements remain clearly defined throughout the evaluation.
Hansen Plastics works with OEMs on material selection, tooling, manufacturability, and production requirements. If your team is reviewing next year’s manufacturing budget, explore our injection molding capabilities or contact Hansen Plastics to discuss opportunities to improve production efficiency while maintaining part performance.